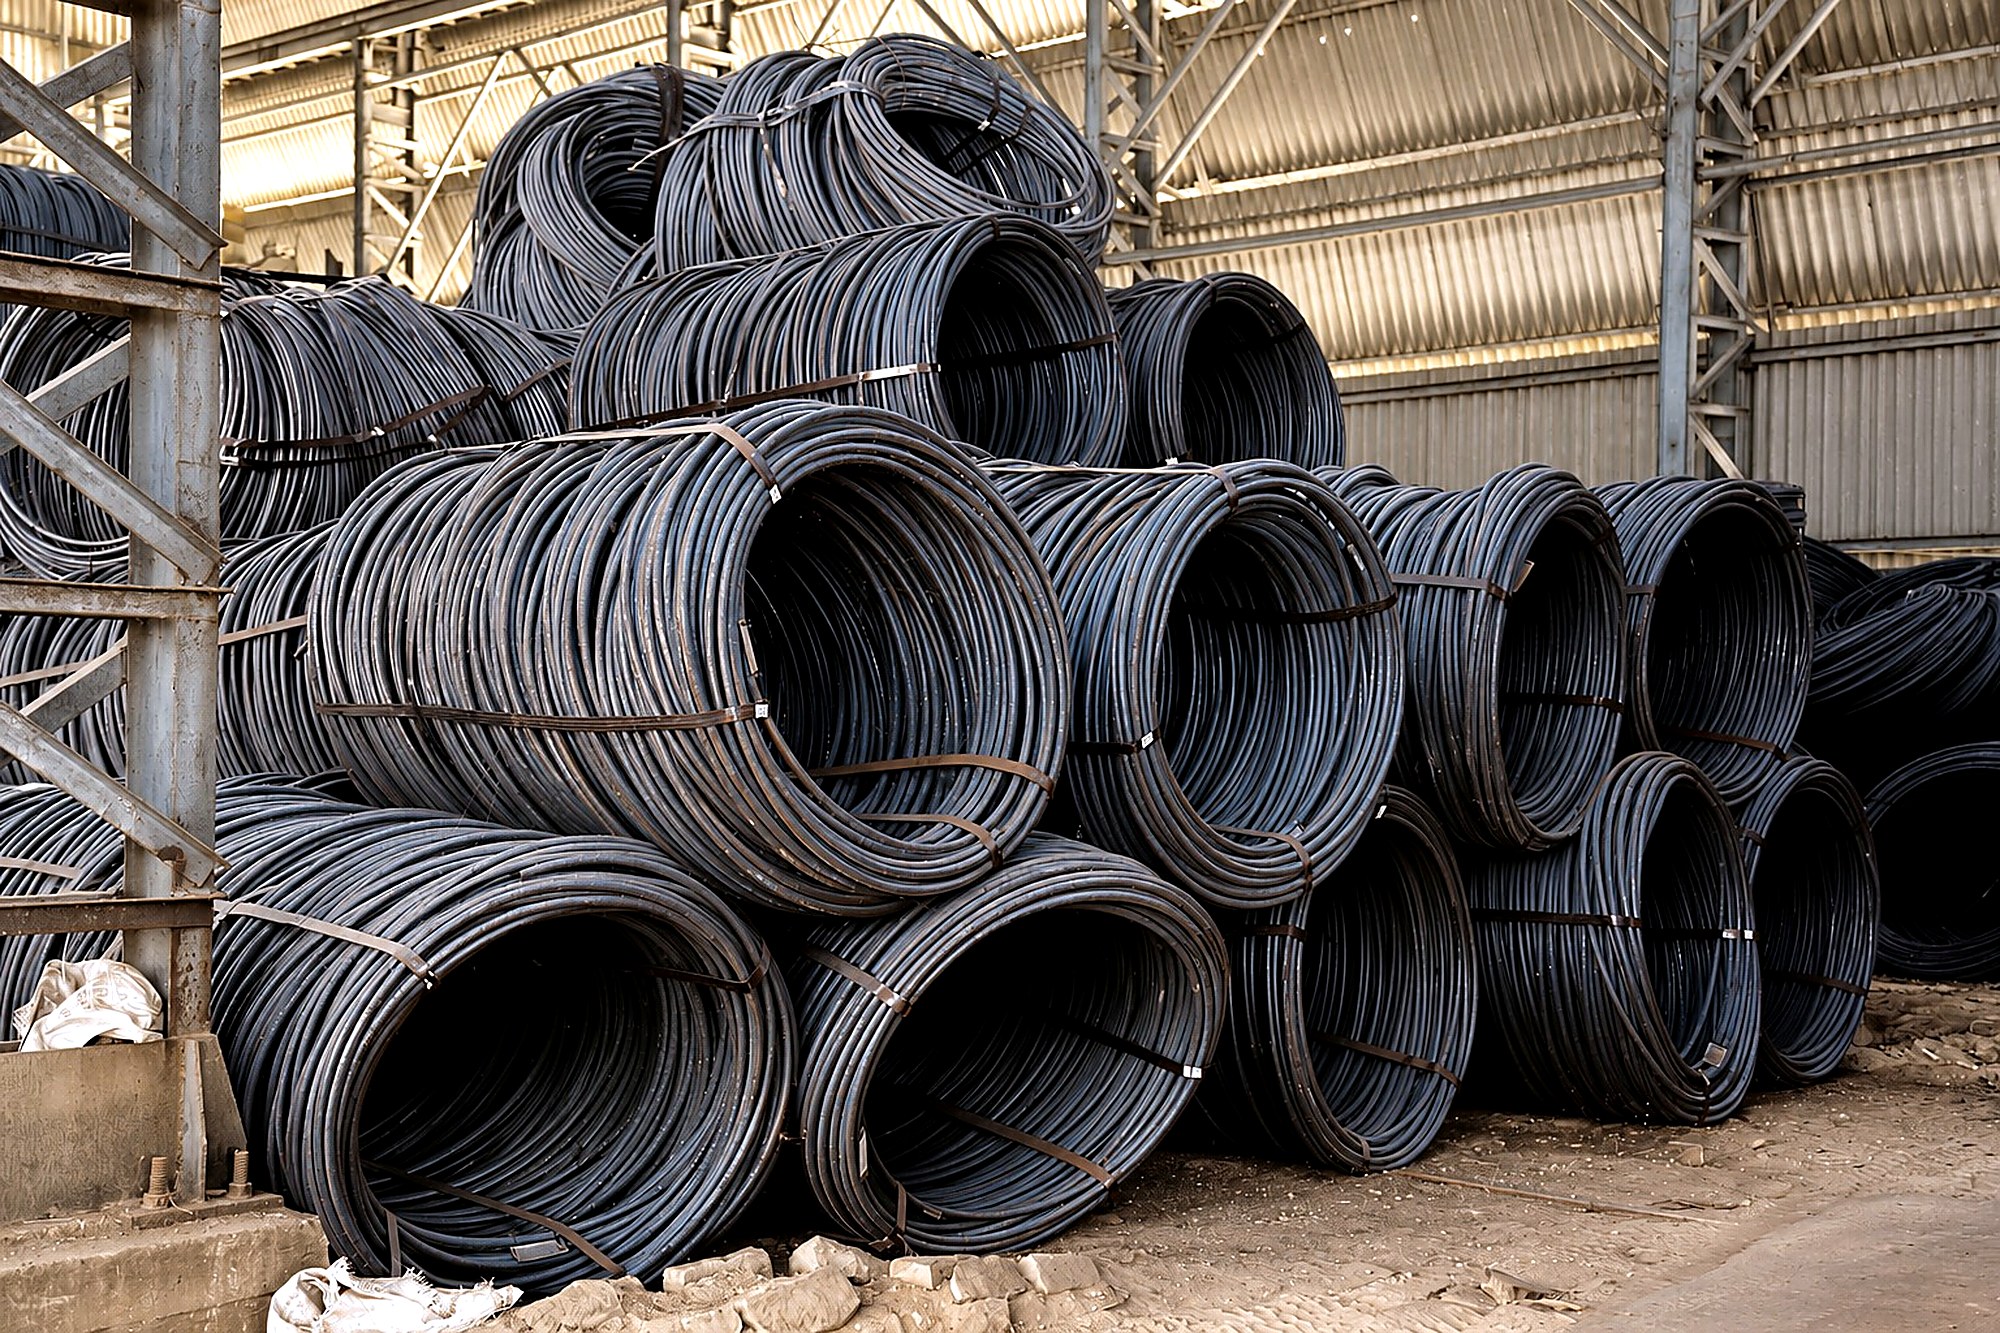
 1 · RM STORAGE
01
Raw material storage
Wire rod and bar stored by SAE grade and colour-coded (1008 to 4140 / 41Cr4), every bar marked with its heat number.
every bar marked with its heat numberTwo units at Sankrail, Howrah take wire rod through forging, threading, heat treatment, coating and NABL testing without the material ever leaving our gates. We work to RDSO, POWERGRID and BIS standards, because every joint we make carries the nation's traffic and power.
One factory controls all nine steps, so no problem is handed to someone else.
1 · RM STORAGEWire rod and bar stored by SAE grade and colour-coded (1008 to 4140 / 41Cr4), every bar marked with its heat number.
every bar marked with its heat number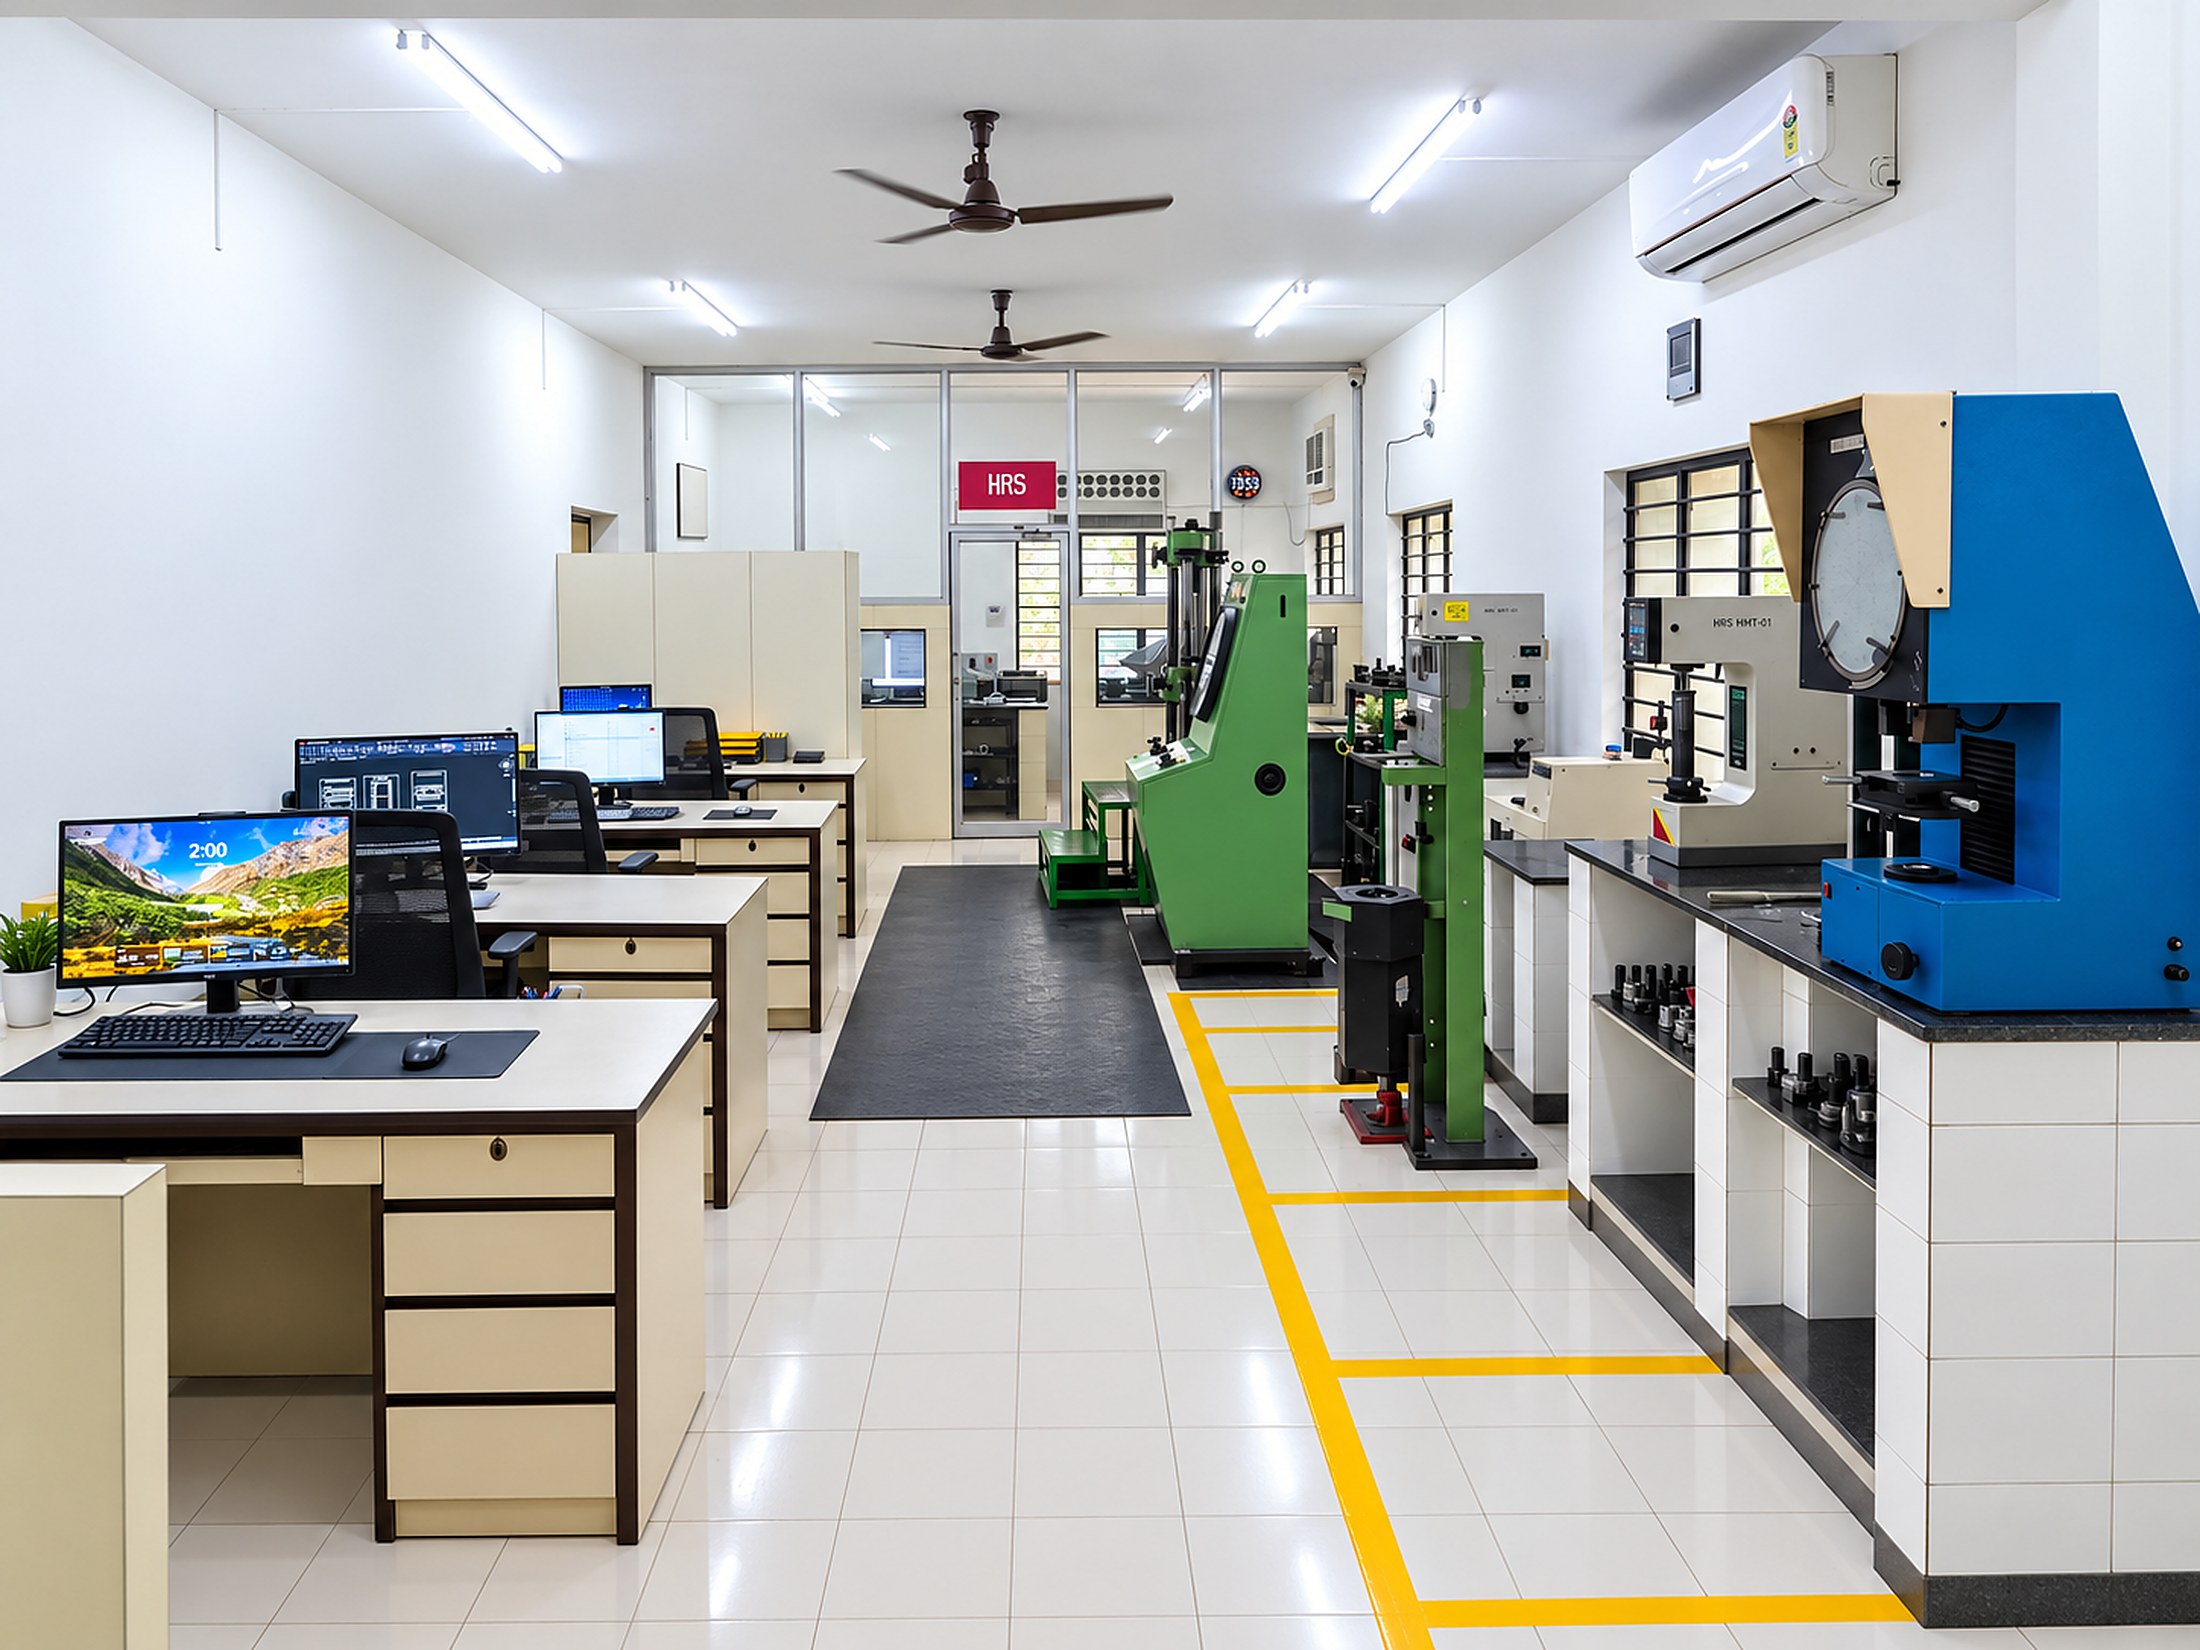 2 · TESTING
German spectrometer checks every heat against the mill certificate before it is released to production.
German spectrometer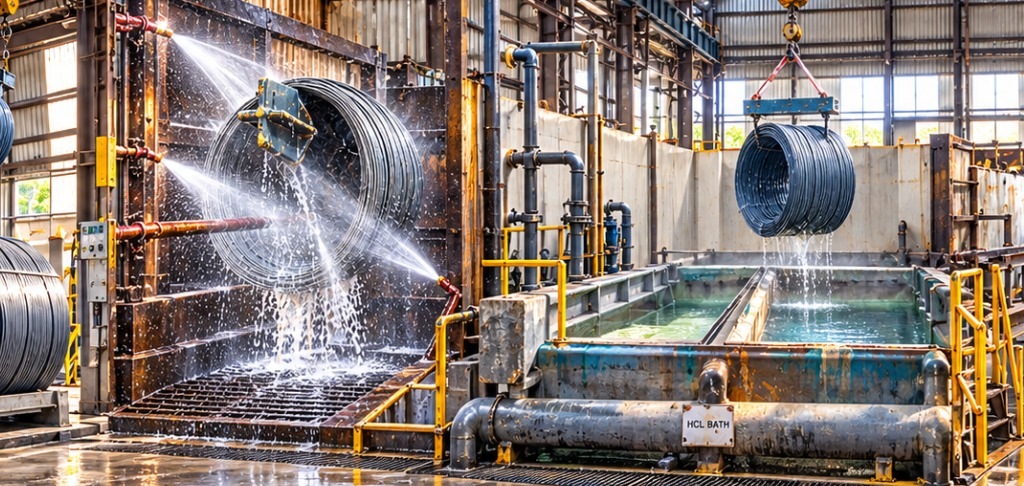 3 · WIRE PROCESSING
Pickling, phosphating and wire drawing in Unit II, so the forging line never waits on outside job-work.
wire drawing in Unit II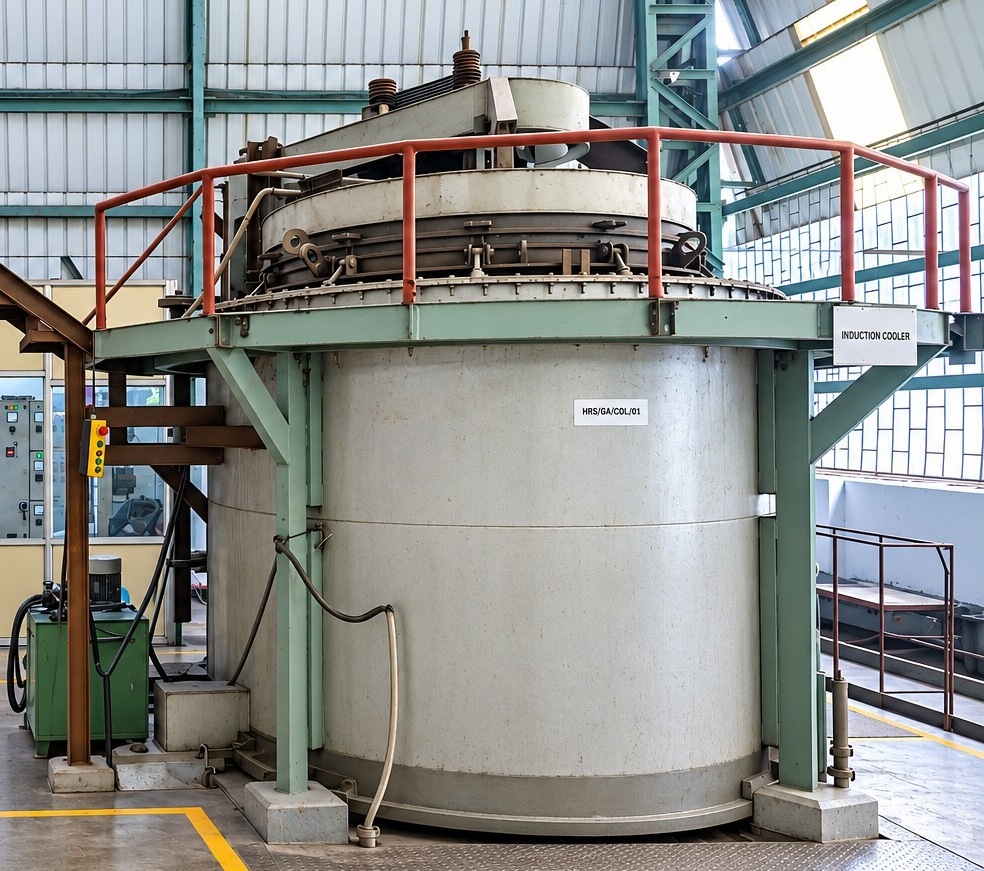 4 · ANNEALING
Our own annealing furnace prepares wire for cold forging of high-strength grades.
cold forging of high-strength grades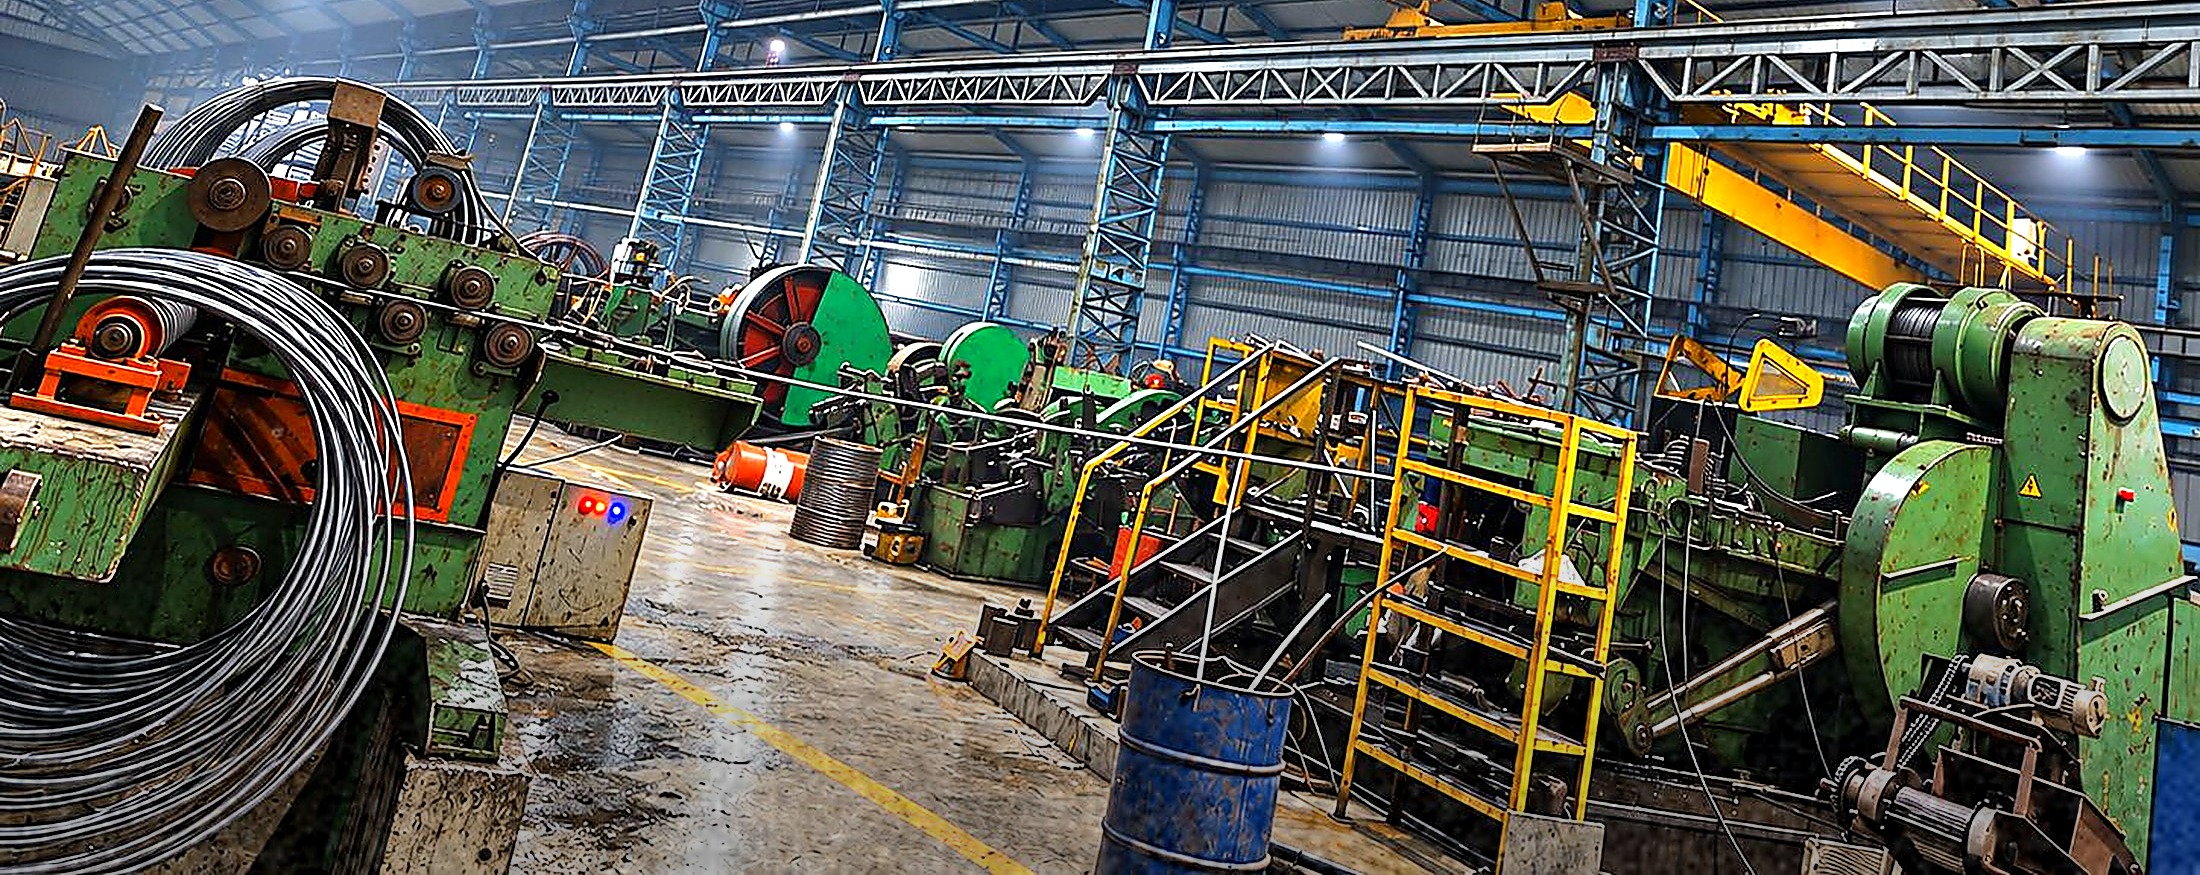 5 · FORGING · UNIT II
Bolts cold forged to M30 and hot forged to M48; heavy hex nuts cold forged to M27 and hex nuts to M30 on National and San Shing formers.
National and San Shing formers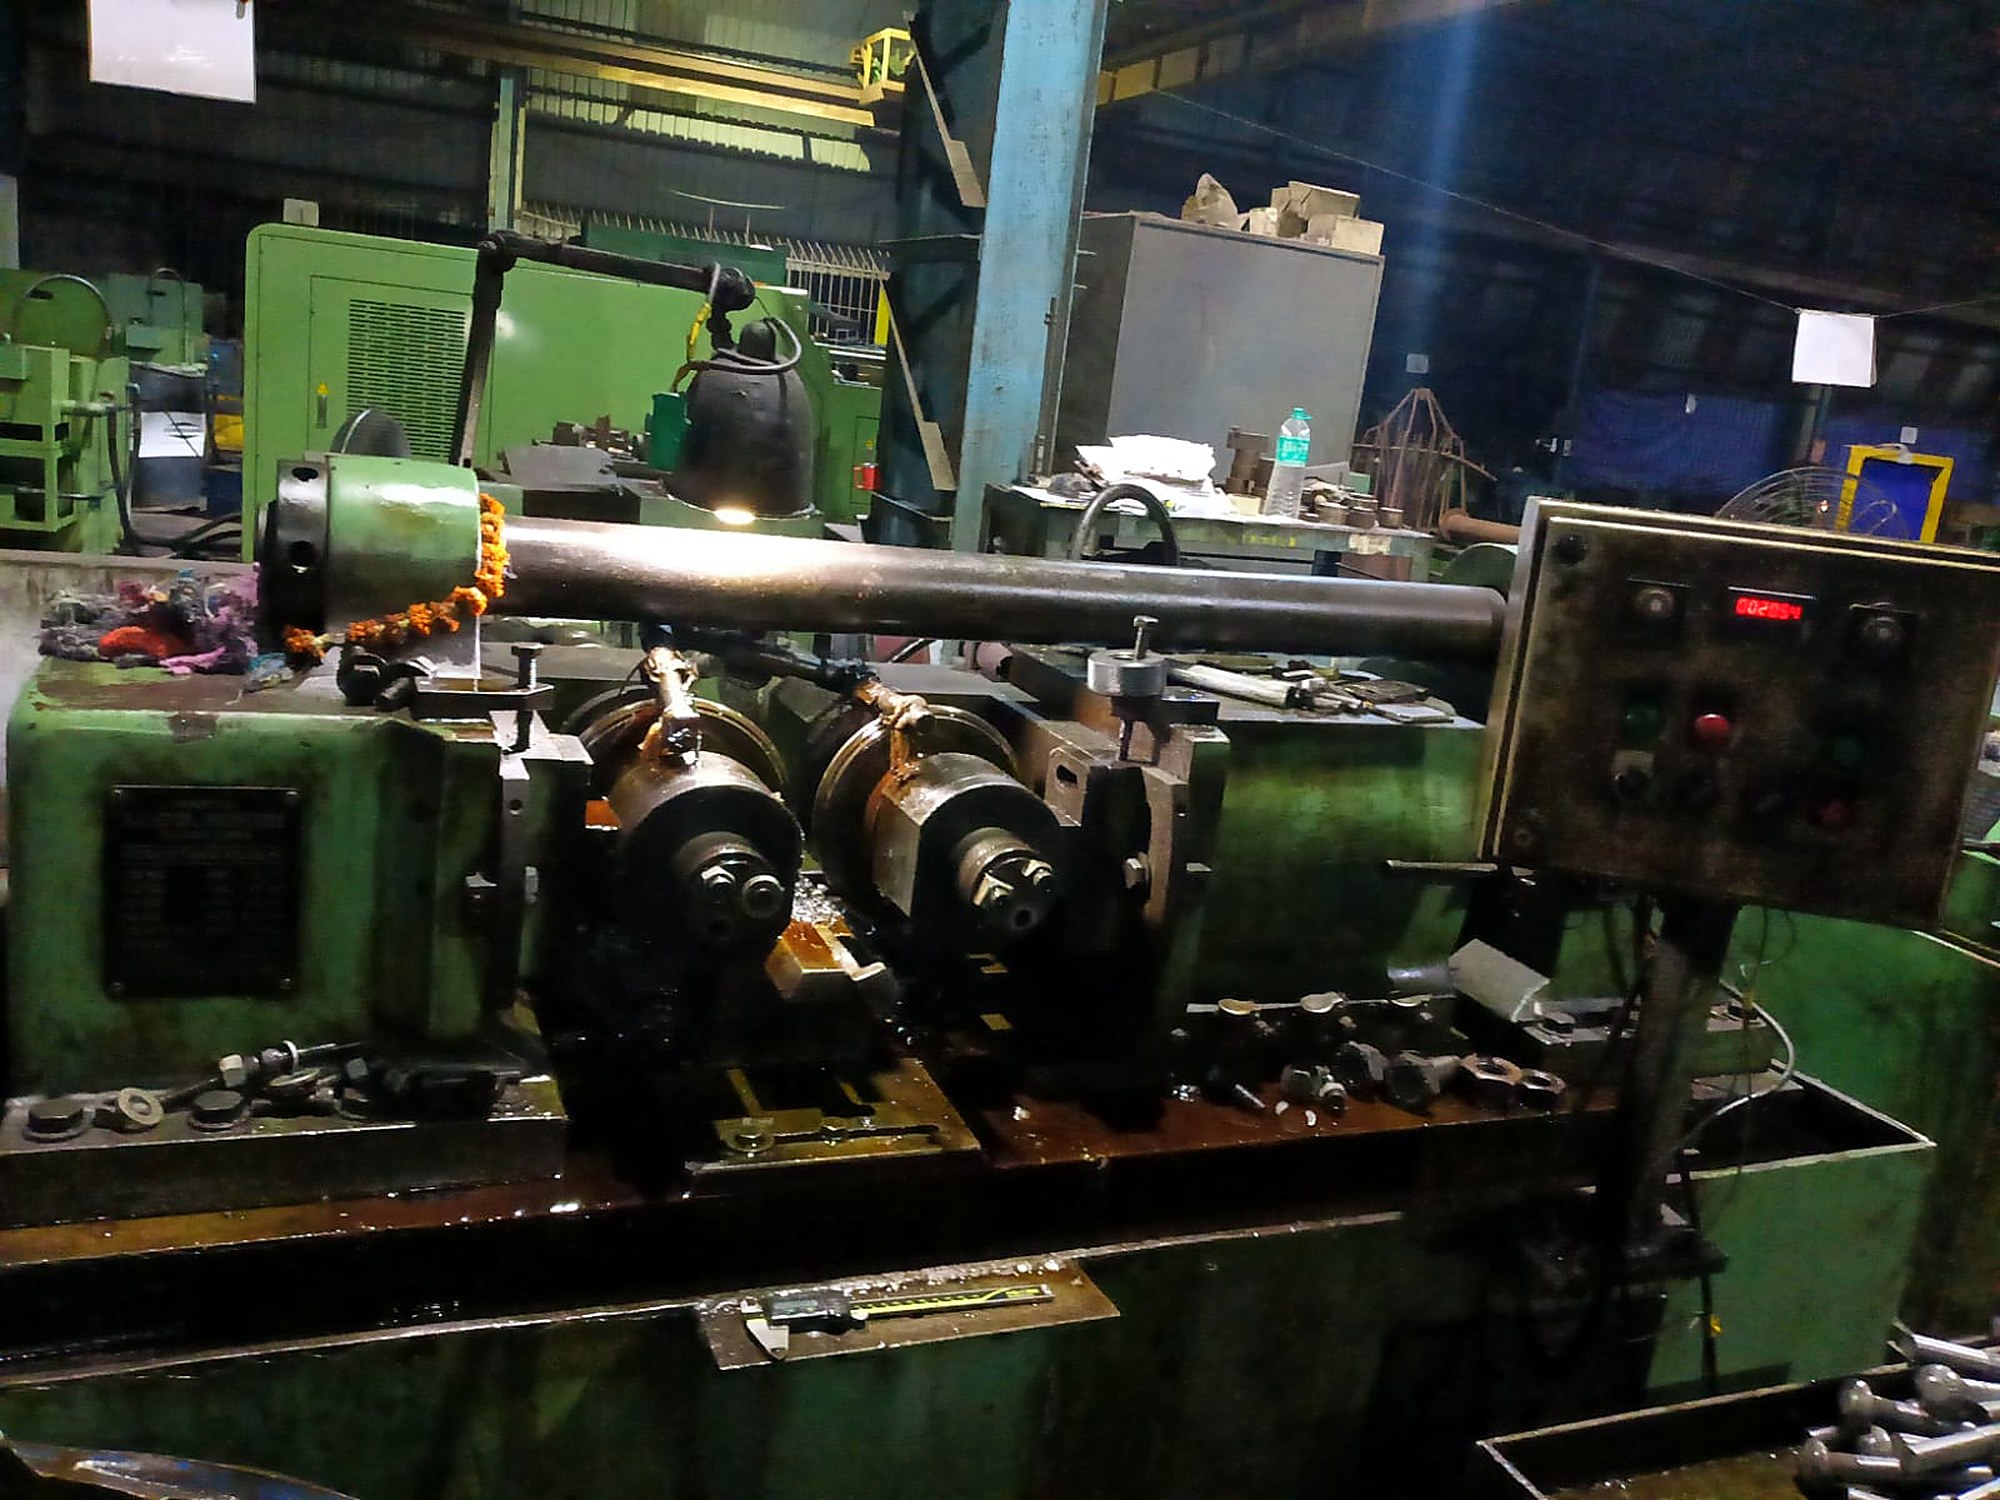 6 · THREAD ROLLING M80
Hydraulic thread rolling up to M80, so the grain follows the thread form.
Hydraulic thread rolling up to M80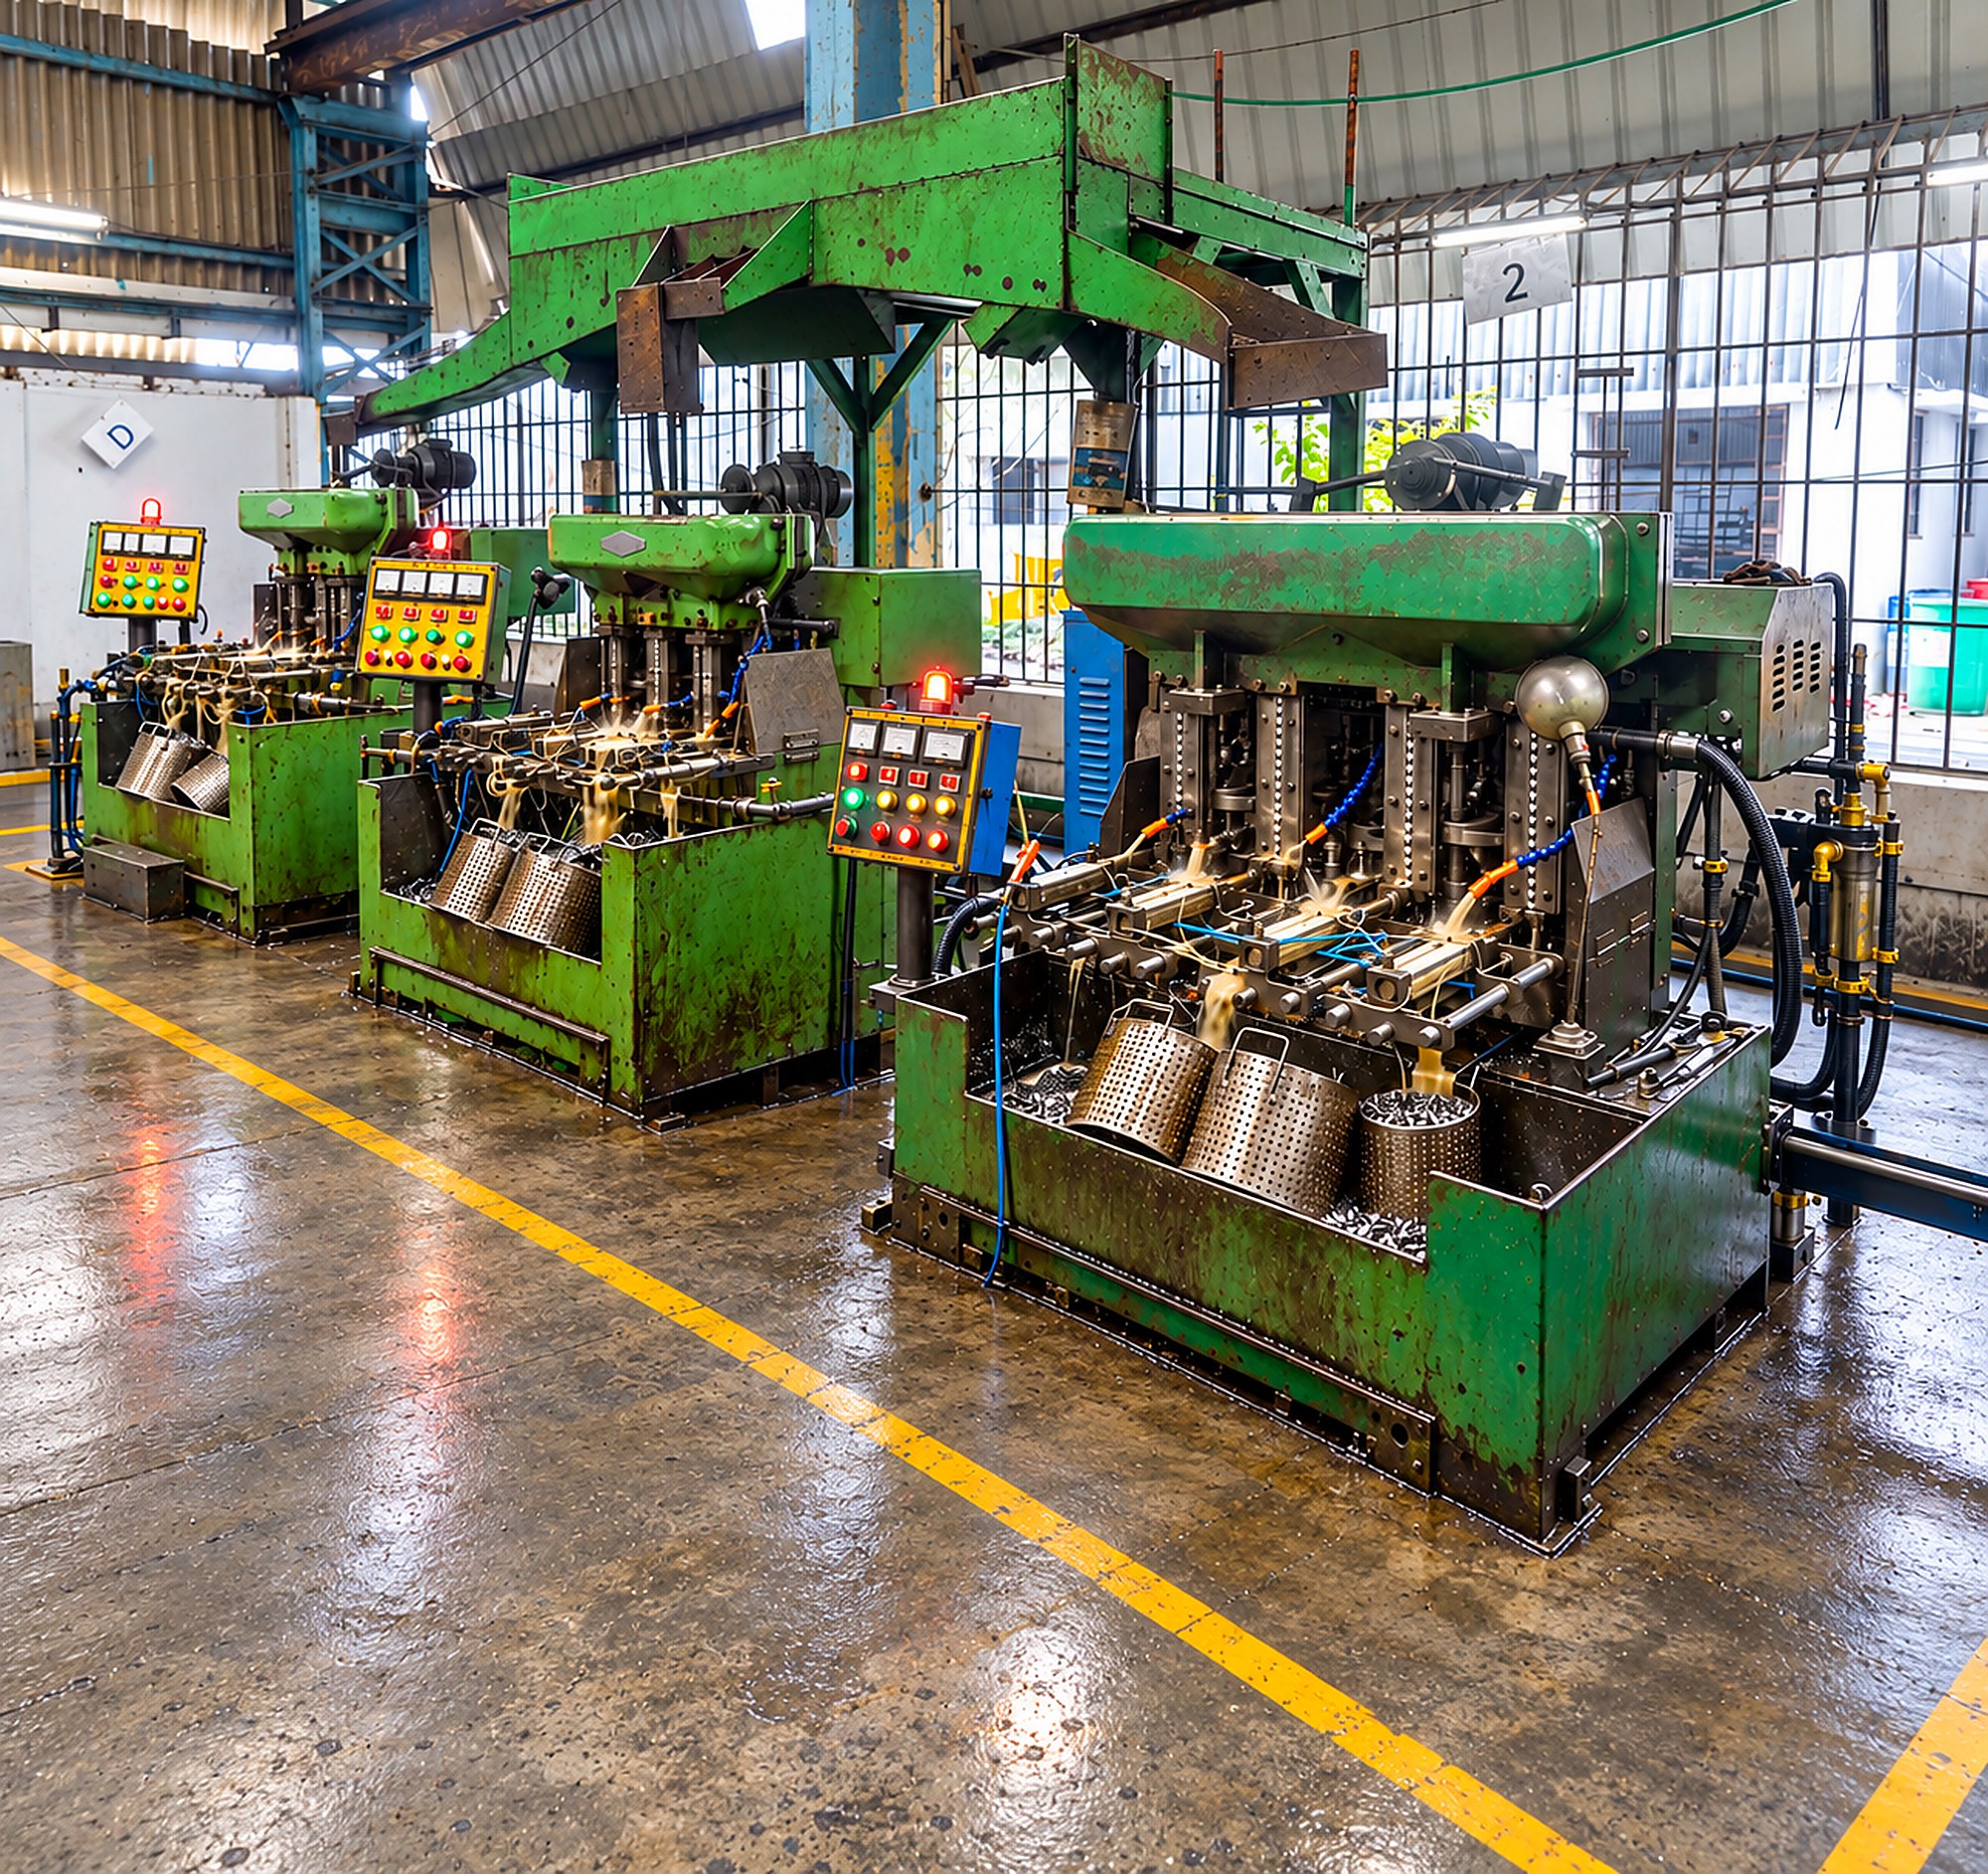 7 · NUT TAPPING
Nut tapping lines for standard and heavy hex nuts, with gauges checked every shift.
gauges checked every shift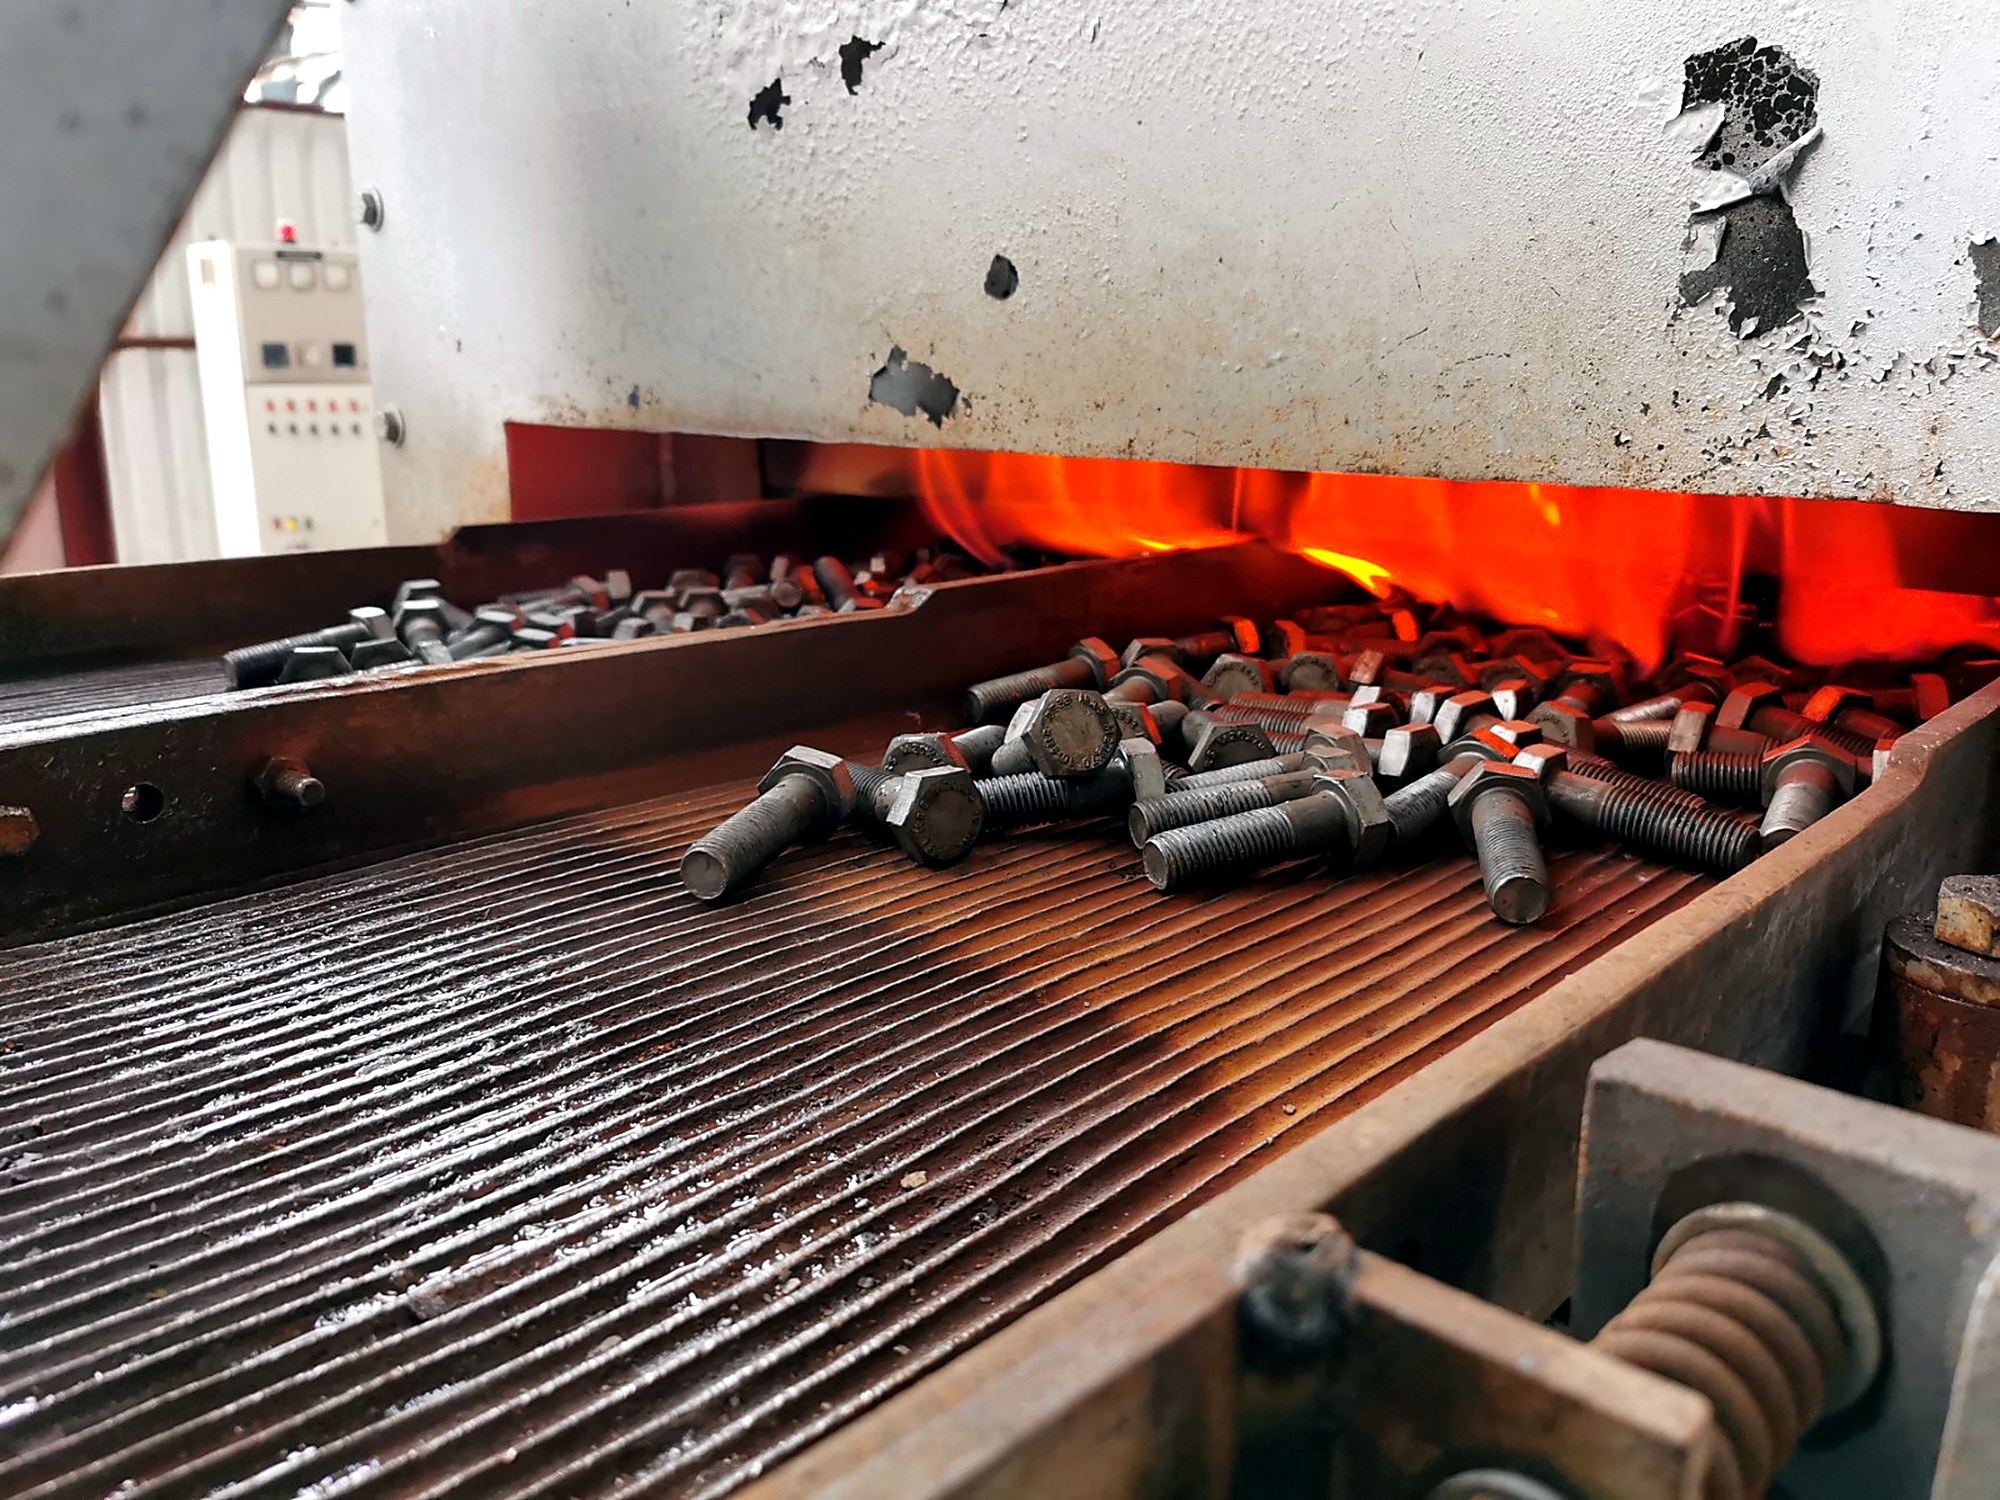 8 · HARDEN & TEMPER
Continuous hardening and tempering line plus shaker-hearth, rotary and pit furnaces, every batch logged against its heat number.
every batch logged against its heat number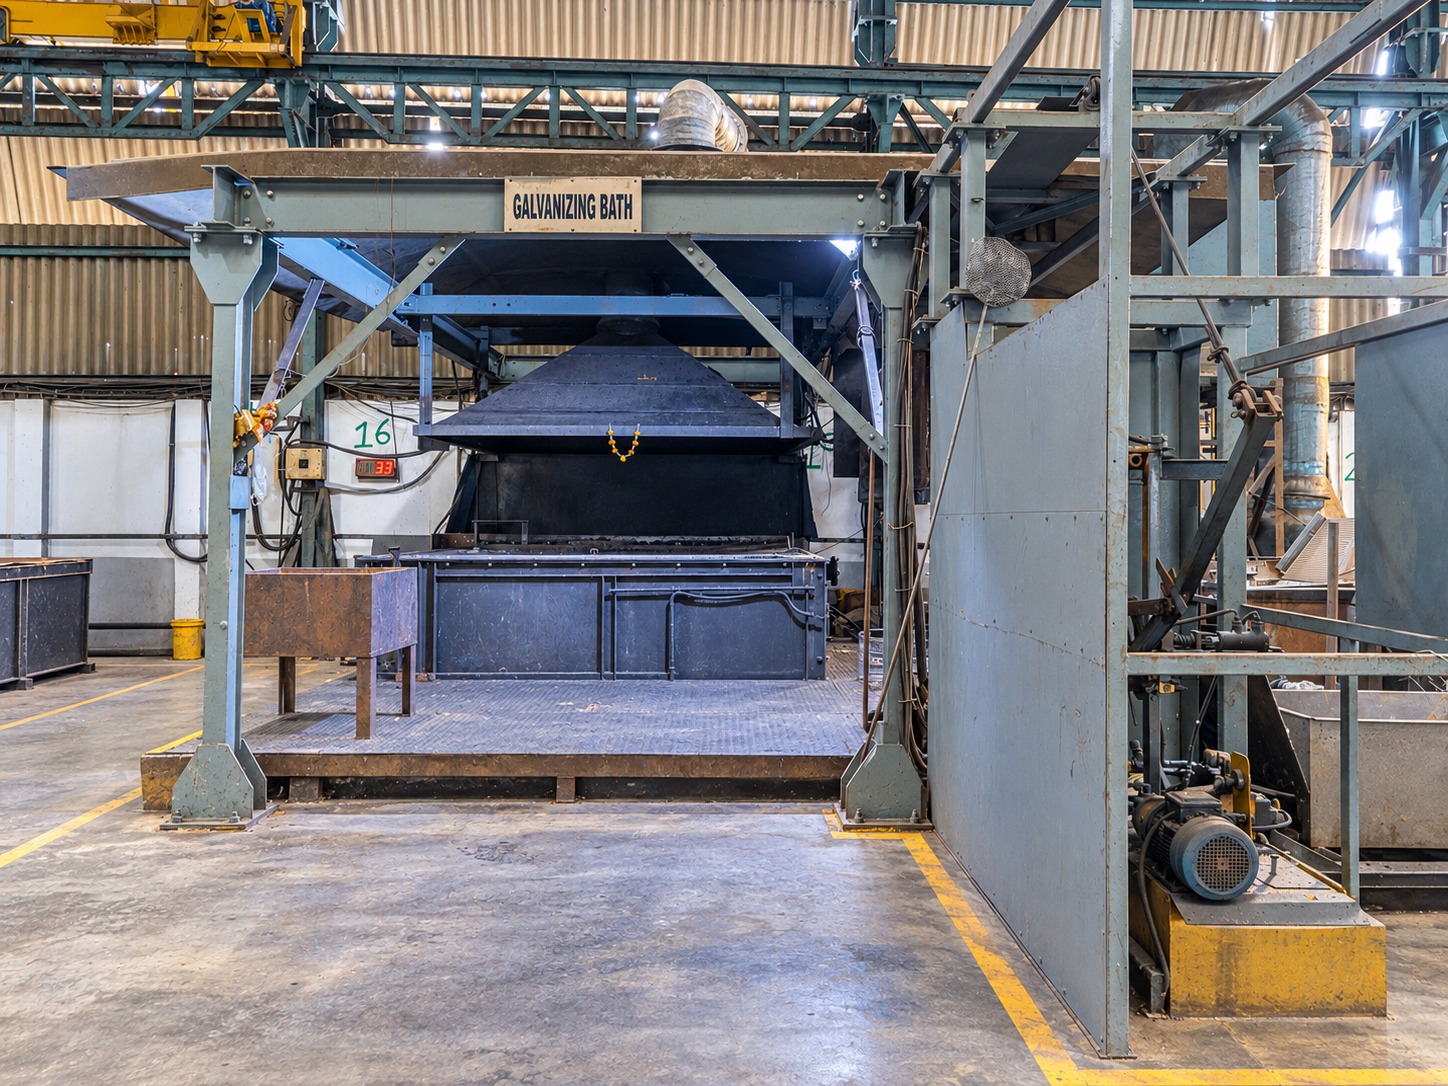 9 · GALVANIZING BATH
Hot-dip galvanizing 25 MT/day in-house, with zinc phosphating 15 MT/day and zinc plating 10 MT/day.
Hot-dip galvanizing 25 MT/day in-houseOne number, start to finish. Heat number on the rod, the route card, the test report and the box.
Traceability · wire rod to wagon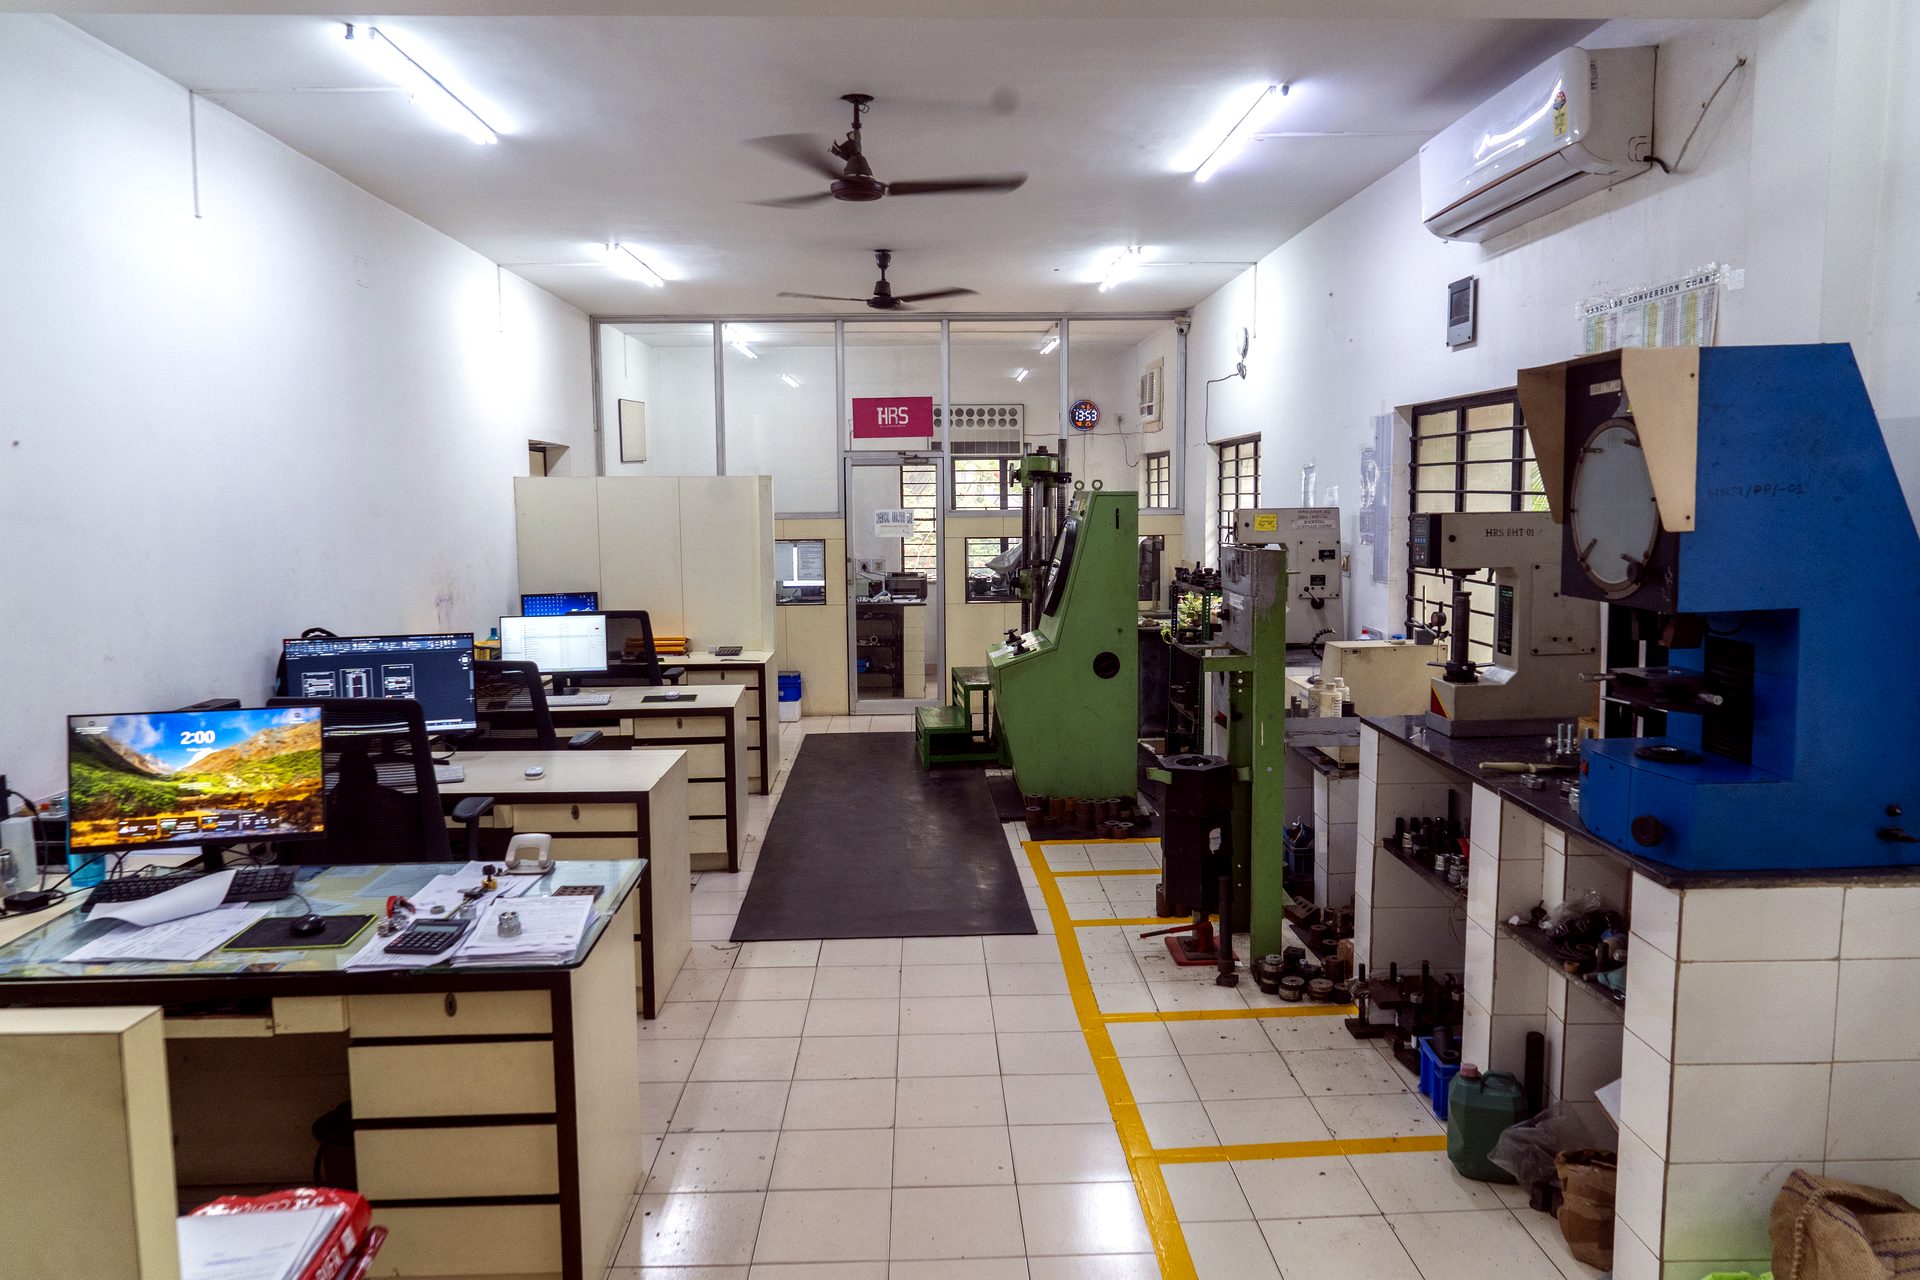 HRS NABL-ACCREDITED LABORATORY · UTM, HARDNESS, IMPACT, PROFILE PROJECTOR
Every lot is tensile, proof-load and hardness tested in our own NABL lab, and traced by heat number from wire rod to carton.
Wire rod and bar come only from integrated steel mills with mill test certificates. On arrival every bar end is colour-coded by grade and marked with its heat number, and our spectrometer checks the chemistry against the certificate before anything goes to the formers. That heat number follows the lot through forging, heat treatment, coating and testing, onto the tag on every bag and box.
Bar ends painted by grade
Heat number written on every bar
From wire rod to wagon
Every lot is tensile, proof-load and hardness tested in our own NABL lab
onto the tag on every bag and box
Inspected and passed by
COMPANY PROFILE 2026 · BOLTS · NUTS · WASHERS · LOCK BOLTS · STUDS · SPECIALS
Select any page to browse. Click the large preview to open that page in the original PDF with full zoom.
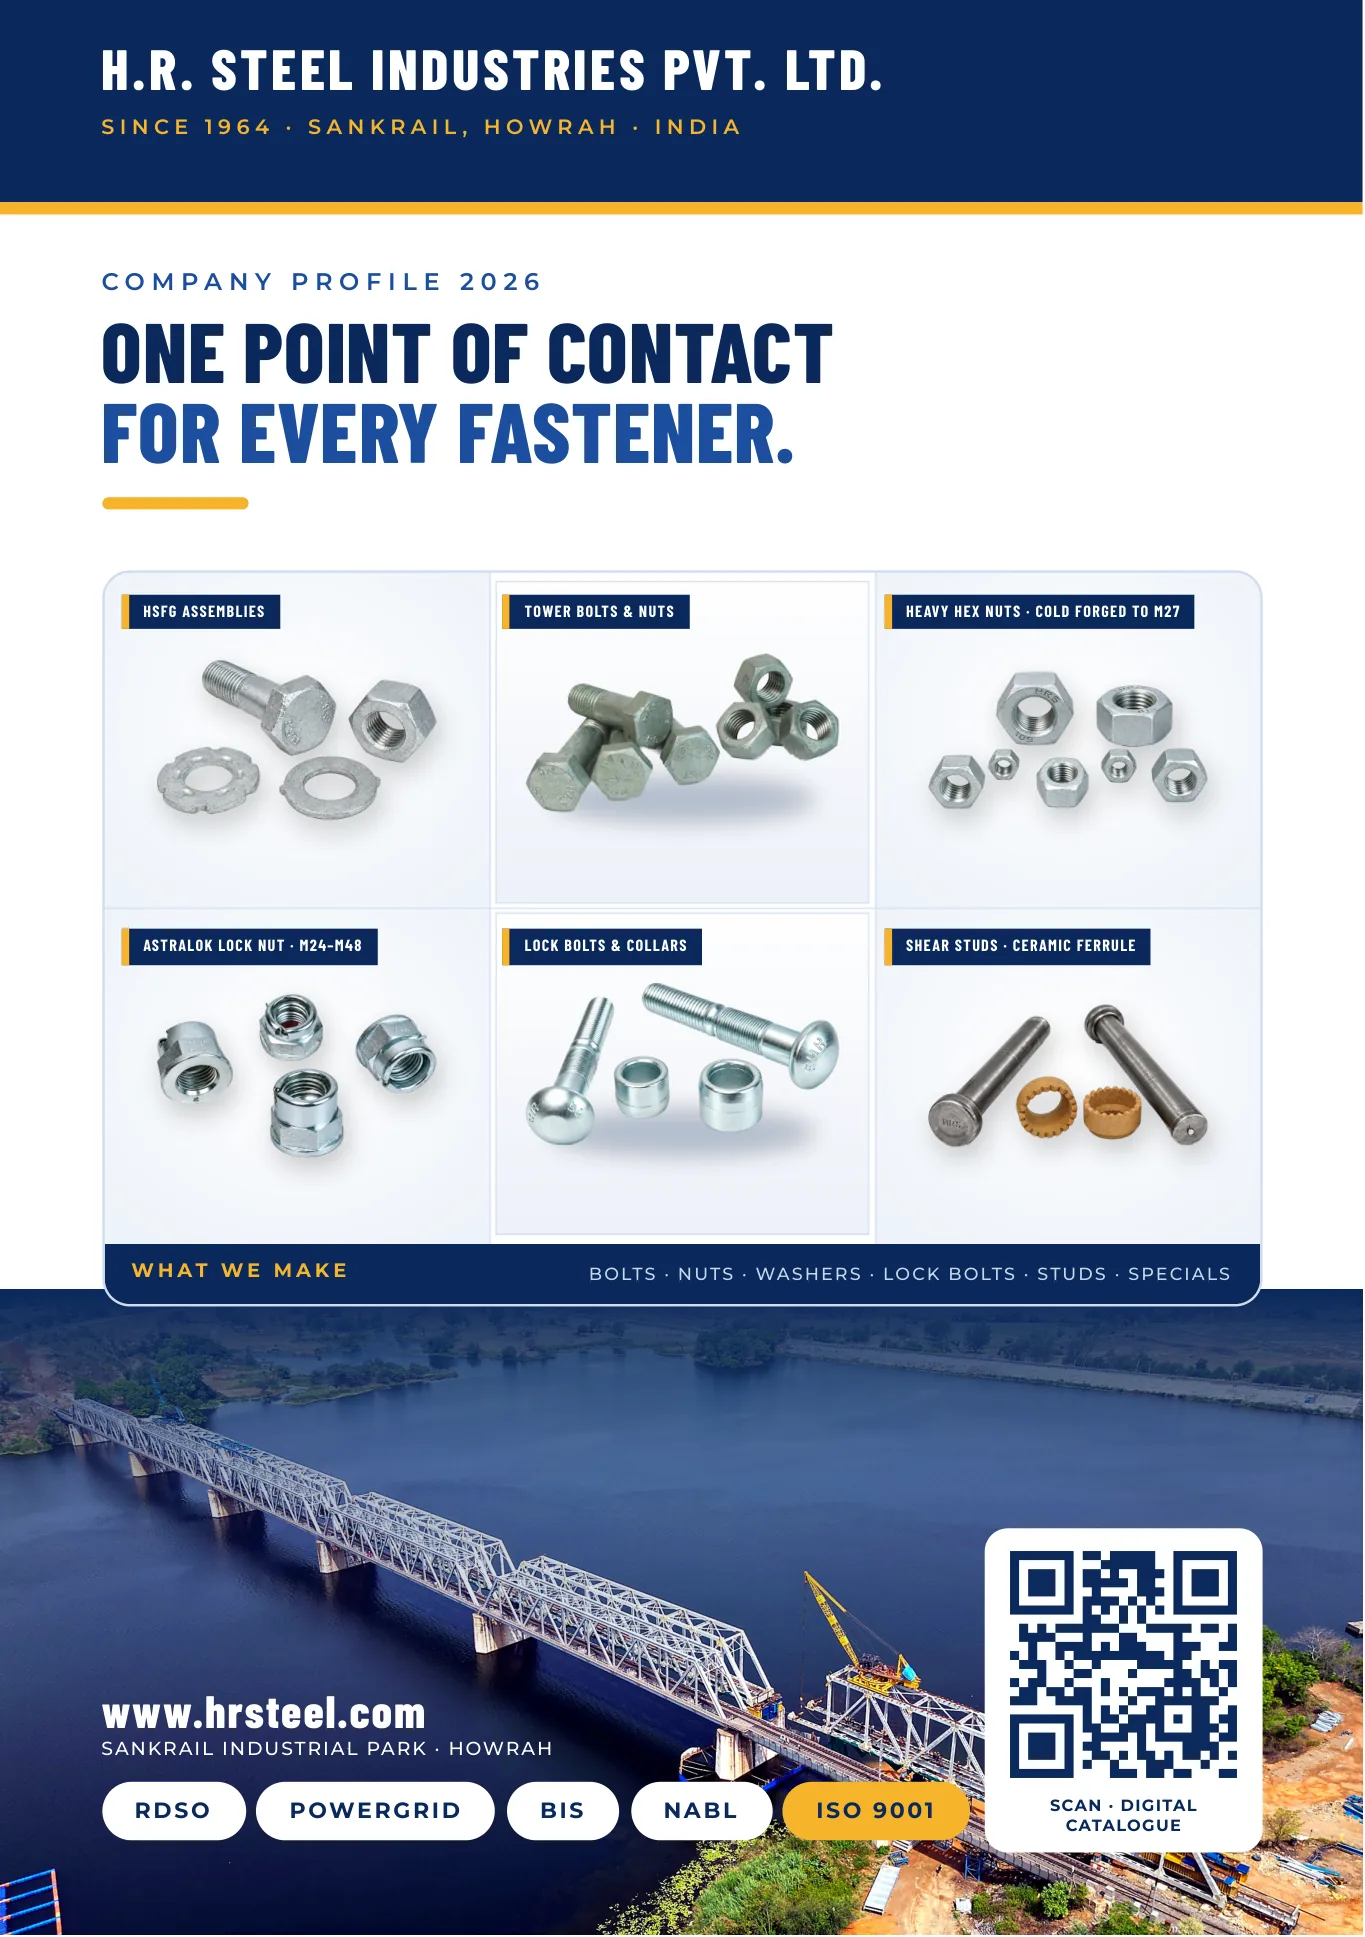
A dedicated R&D department, production team, sales and support team and full supply-chain infrastructure, so what we promise at enquiry is what arrives at your site.